What Is the Best Cereal Bar Production Line in China?
Choosing the best Cereal Bar Production Line in China requires more than comparing machine prices. A reliable line must match your recipe, capacity, bar size, and packaging method. It should handle oats, nuts, dried fruit, syrups, and other ingredients without damaging their texture.
In practical evaluations, we examine mixing consistency, forming accuracy, cooling performance, cutting precision, and packaging stability. A good line should produce clean edges and uniform weights, even during long operating shifts. Stainless steel contact parts, accessible cleaning areas, and clear control panels also support safe daily production. These details matter on a busy factory floor.
Supplier experience is equally important. Established manufacturers can provide factory testing, installation guidance, operator training, spare parts, and responsive technical support. Buyers should request production videos, sample testing, electrical specifications, and references from similar cereal bar producers. Certification claims should be checked carefully, rather than accepted without evidence.
There is no universal winner.
The best choice depends on your actual production plan. A small brand may need a flexible, semi-automatic system, while a large manufacturer may prioritize high-speed forming and integrated wrapping. Some lines appear impressive but perform poorly with sticky mixtures or frequent recipe changes. This is an easy detail to overlook. Therefore, this guide compares Chinese production lines through measurable performance, long-term reliability, maintenance needs, and total operating value. It also recognizes an uncomfortable truth: even advanced equipment cannot fix an unstable formula or poorly trained operators.
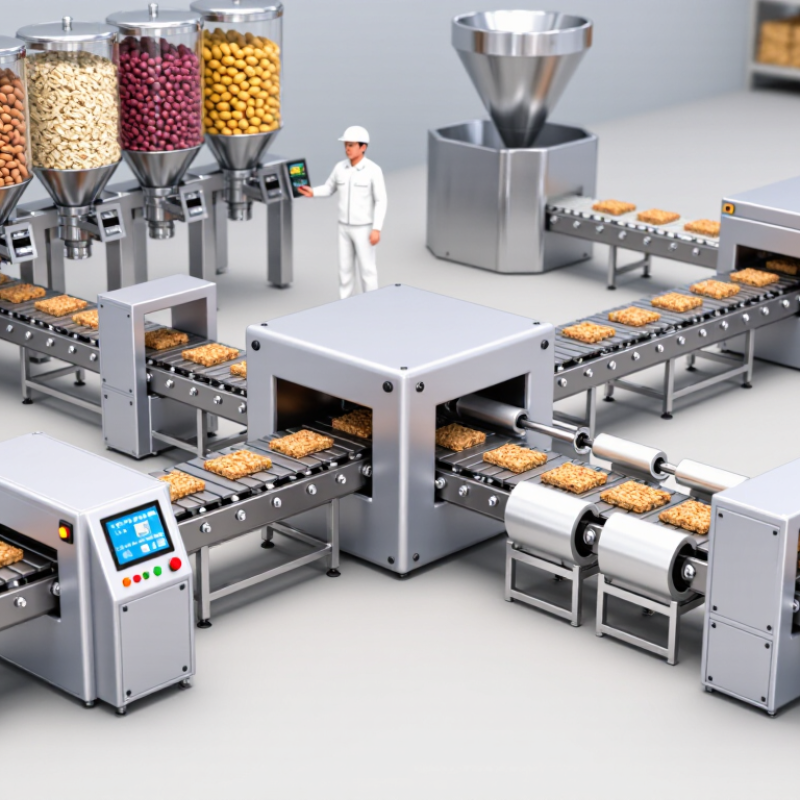
China’s Cereal Bar Market: Capacity, Formats, and 2024 Industry Data
What Is the Best Cereal Bar Production Line in China?
China’s Cereal Bar Market: Capacity, Formats, and 2024 Industry Data
China’s cereal bar market became more diverse in 2024. Consumers increasingly chose oat bars, nut bars, fruit-filled bars, and reduced-sugar recipes. Public industry reports show steady demand, but reported market values vary widely. Different research methods explain much of this gap.
Capacity depends on product format and factory size. A compact line may produce 300–500 kilograms per hour. Medium lines commonly handle 800–1,500 kilograms per hour. Larger systems can exceed 2,000 kilograms per hour with stable material feeding. These figures require suitable ingredients, trained operators, and consistent recipes. Output alone does not define the best line.
A practical line usually includes mixing, cooking or binding, slab forming, cooling, cutting, and packaging. For soft fruit bars, a controlled depositing system may work better than standard slab forming. For crunchy nut bars, accurate syrup cooking matters more. Buyers should inspect cutting accuracy, cooling temperature, cleaning access, and energy use. A small test batch reveals more than a sales brochure.
In my experience, factories often overestimate future capacity. This creates unused equipment and difficult maintenance. Some buyers also ignore packaging changes between 20-gram bars and larger family packs. That mistake is expensive. The best Chinese production line is therefore the one matching current recipes, target formats, labor skills, and realistic 2024 demand data.
Ingredient Dosing: ±1% Accuracy and Codex-Compliant Process Control
What Is the Best Cereal Bar Production Line in China?
Choosing the best cereal bar production line in China starts with ingredient dosing, not stainless steel appearance. A reliable system measures grains, syrups, oils, fibers, and micronutrients with target accuracy of ±1%. That tolerance matters. A small dosing error can change texture, sweetness, allergen control, and declared nutrition values. Load cells, calibrated hoppers, and recipe-controlled feeders help operators repeat each batch. Manual checks still matter.
In practice, the line should record every ingredient lot, weighing result, adjustment, and operator action. This creates traceability from receiving to finished bar. Codex-aligned process control should support hygienic design, hazard analysis, sanitation verification, and documented critical limits. It should also manage heating time and temperature, because syrup viscosity affects cutting and binding. Sensors need calibration schedules. Software needs access control. A clear alarm is better than a hidden deviation.
During factory acceptance testing, request several trial batches with different moisture levels and inclusions. Measure actual weights, not only screen displays. Ask technicians to test start-up, changeover, cleaning, and short interruptions. These details reveal whether ±1% accuracy survives real production pressure. No line is perfect. Dust, sticky syrup, and rushed operators can expose weak points. I would also review maintenance access and spare-part availability before approval. A technically impressive machine may still disappoint if cleaning takes too long.
Seven Production Stages: Mixing, Forming, Baking, Cooling, Cutting, Packing
What Is the Best Cereal Bar Production Line in China?
The best cereal bar production line is not simply the fastest. It must control texture, weight, hygiene, and product waste. Grand View Research estimated the global cereal bar market at over USD 11 billion in 2023, with continued growth expected through 2030. That growth increases pressure on Chinese manufacturers to deliver stable, export-ready production.
The process begins with accurate ingredient dosing and mixing. Oats, syrups, nuts, and dried fruit need even distribution. Forming then creates consistent thickness and density. Baking must control temperature and moisture, or the bars may become hard or fragile. Cooling is often underestimated. A gradual temperature drop protects shape and reduces condensation. Cutting should produce clean edges with minimal crumbs. Inspection adds the seventh stage, including weight checks and metal detection. Packing follows, using sealed film to protect freshness and prevent contamination.
Real factory trials matter more than catalog speed. PMMI’s 2024 packaging machinery report highlights labor efficiency, flexible changeovers, and automation as major investment priorities. These points support servo control and recipe management, especially for different bar sizes. HACCP principles from the FAO and WHO Codex framework should guide sanitation and hazard control. A perfect line does not exist. Product stickiness, seasonal humidity, and cleaning time still create surprises. That assumption needs testing. A practical evaluation should measure yield, downtime, moisture variation, and changeover minutes before purchase.
What Is the Best Cereal Bar Production Line in China?
Seven production stages: ingredient preparation, mixing, forming, baking, cooling, cutting, and packing.
This reference chart shows typical residence time by stage in a continuous cereal bar production process. Cooling generally requires the longest time to stabilize product structure before cutting, while forming and cutting are designed for rapid, continuous operation.
Food Safety Standards: GB 14881, GB 2760, HACCP, and ISO 22000
Choosing the best cereal bar production line in China starts with food safety, not output speed. A reliable line should support GB 14881 through hygienic zoning, washable surfaces, controlled personnel flow, and documented sanitation. Product-contact parts must resist corrosion and avoid hidden powder traps. In real factory audits, small gaps around conveyors often become difficult cleaning points. That detail matters.
GB 2760 controls permitted food additives and their use limits. The formulation team should verify every syrup, flavor, vitamin, and processing aid against the current standard. Automated dosing improves consistency, but it does not replace ingredient approval or batch records. HACCP maps hazards from weighing and roasting to cooling, cutting, and wrapping. Critical limits need practical monitoring, not paperwork alone. A metal detector, temperature log, and allergen changeover check provide useful evidence. Still, one missed record weakens the whole system.
Tips: Ask for cleaning validation records, calibration certificates, allergen-control procedures, and traceability tests. Request a trial run with your actual cereal mix. Observe dust control and operator handwashing. Confirm whether rejected bars are isolated and recorded. ISO 22000 can connect these controls through internal audits and corrective actions. Certification is valuable, but daily behavior is the real test. Sometimes the fastest line is not the safest choice. Good engineering leaves fewer opportunities for human error.
Selecting the Best Line: 500–2,000 kg/h Capacity, OEE, Energy, and ROI
What Is the Best Cereal Bar Production Line in China?
Selecting a cereal bar line starts with the product, not the advertised speed. A 500 kg/h system may suit varied recipes and frequent changeovers. A 2,000 kg/h system fits stable, high-volume production. However, rated capacity can hide losses. Sticky syrups, uneven cooling, and manual packing often reduce real output. During factory evaluations, I would request hourly production records, not only brochure figures.
OEE offers a clearer comparison. Ask for availability, performance, and quality data from similar cereal bars. An 85% OEE target is useful, but it should be verified under your recipe. Check temperature control, slab thickness, cutting accuracy, and restart time. Small defects matter. A three-millimeter size variation can create packaging waste and customer complaints. Operators should also demonstrate a complete cleaning and changeover cycle.
Energy performance directly affects ROI. Review heater power, cooling load, compressed-air demand, and standby consumption. A high-capacity line is not automatically economical. Calculate payback using actual labor, waste, maintenance, utilities, and saleable output. Include spare parts and operator training. I would also test a pilot batch before signing. Laboratory results may look excellent, yet production can reveal brittle bars or poor flow. The best choice is the line that maintains stable quality at a realistic speed, not the one with the largest number on its nameplate.
What Is the Best Cereal Bar Production Line in China? - Selecting the Best Line: 500–2,000 kg/h Capacity, OEE, Energy, and ROI | Line Configuration | Nominal Capacity
(kg/h) | Recommended Operating Rate
(kg/h) | Expected OEE
(%) | Specific Energy Use
(kWh/t) | Installed Electrical Load
(kW) | Indicative CAPEX
(USD) | Estimated Payback
(Years) | Best-Fit Application |
| Compact Entry Line | 500 | 350–425 | 65–72 | 115–145 | 95–125 | 250,000–420,000 | 2.5–3.5 | Pilot production, regional distribution, and multiple recipe testing |
| Standard Modular Line | 1,000 | 700–850 | 72–78 | 95–125 | 170–220 | 450,000–750,000 | 2.0–3.0 | Growing brands requiring flexible recipes and consistent retail output |
| High-Throughput Line | 1,500 | 1,050–1,275 | 76–82 | 85–110 | 245–315 | 700,000–1,150,000 | 1.8–2.7 | Established factories serving national retail and food-service contracts |
| Industrial High-Capacity Line | 2,000 | 1,400–1,700 | 78–84 | 80–105 | 320–410 | 1,000,000–1,650,000 | 1.7–2.5 | Large-volume contracts, export production, and multi-shift operation |
| Planning basis: Indicative engineering benchmarks for cereal-bar lines including mixing, slab forming, cooling, cutting, wrapping, and basic conveying. OEE combines availability, performance, and quality; actual results depend on recipe, bar dimensions, moisture, packaging format, staffing, maintenance, and operating schedule. CAPEX excludes building work, taxes, freight, installation, utilities, and customized automation. Payback assumes two 8-hour shifts, 300 operating days per year, stable product demand, and a contribution margin of USD 0.35–0.55 per kg. |

