How to Choose the Right Alloy Powder for Your Needs?
Choosing the right Alloy Powder is a practical engineering decision, not a simple catalog search. The best grade depends on the part, process, equipment, and service environment.
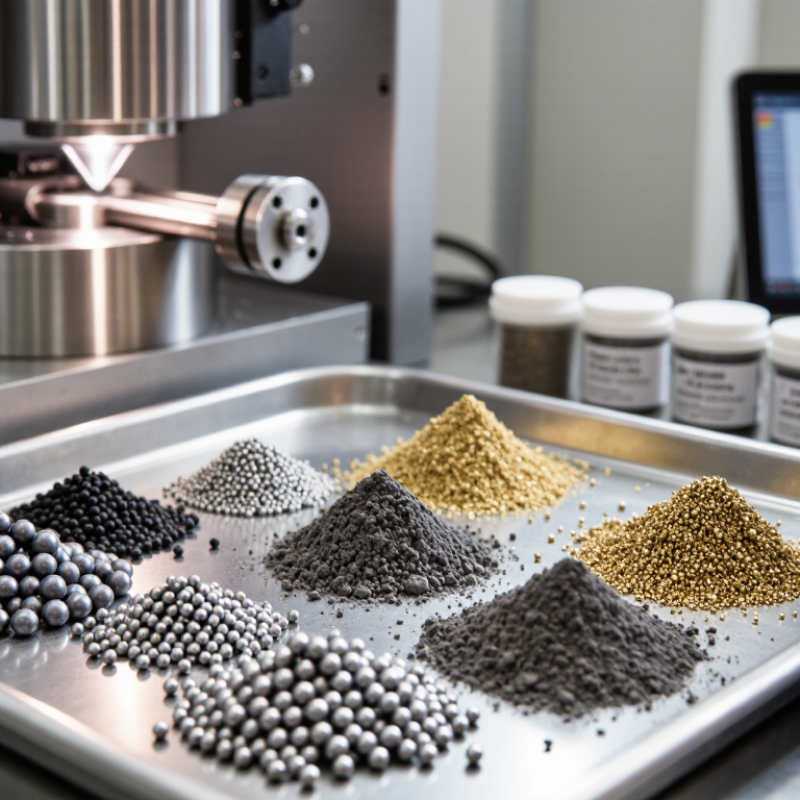
Professor Ma Qian, a recognized metal additive manufacturing expert, captures this principle: “Powder quality must be judged by its behavior in the process, not by chemistry alone.” This view matters on the production floor. A powder may meet its chemical specification yet produce weak layers, uneven spreading, or excessive porosity. Particle size distribution affects packing and melt behavior. Particle shape influences flow through a narrow recoater. Oxygen, moisture, and surface contamination can change performance during thermal processing. Small differences matter.
Start with the application.
For aerospace parts, nickel-based or titanium alloys may require tight traceability and controlled oxygen levels. Stainless steel powder may suit prototypes, tooling, or corrosion-resistant components. Powder for laser powder bed fusion is not automatically suitable for plasma spraying, cold spraying, or metal injection molding. The process changes the requirement.
Review the certificate of analysis, morphology images, apparent density, flow rate, and recycling history. Ask how each batch was tested. Request evidence from similar equipment, not only general laboratory data. This is where supplier experience becomes valuable.
Still, no selection guide replaces a controlled trial. I have seen technically impressive powders underperform after storage or parameter changes. That uncomfortable possibility deserves attention. A cautious plan compares two qualified grades, records results, and checks the finished part, not merely the powder container. The right Alloy Powder is the one that delivers repeatable performance, verified quality, and sensible total cost.
Define Application Needs: Strength, Heat, Corrosion, and Alloy Family
Choosing the right alloy powder starts with the application, not a supplier catalogue. Describe loads, temperature, moisture, and production method before comparing alloy families. A component under repeated impact needs more than high hardness. It may also require toughness. That helps resist cracking around thin sections. For a heat shield, oxidation resistance and dimensional stability may matter more than room-temperature strength. Record peak temperature, exposure time, contact materials, and maintenance intervals.
Corrosion deserves a realistic test. Salt spray, acidic condensate, and trapped moisture create different damage patterns. Do not assume a corrosion-resistant family suits every environment. Nickel-, iron-, aluminum-, and cobalt-based powders balance strength, heat performance, weight, and cost differently. Particle size and morphology also affect flow, packing, melting, and surface finish. In additive manufacturing, uneven spreading may produce defects even when the chemistry looks suitable. That detail is easy to miss.
Tips: Compare certified chemistry with the required specification. Ask for particle-size distribution, oxygen level, flow data, and reuse guidance. Test representative coupons under real thermal and corrosive conditions. Small trials reveal uncomfortable truths. I prefer recording failed samples rather than hiding them. However, laboratory results still need production-scale confirmation, because handling and machine settings can change performance. Revisit the alloy choice when loads, temperature, or surface exposure changes.
Scores are comparative application-fit ratings from 0 to 100, based on representative properties of commonly used alloy families. Strength reflects typical yield-strength potential, heat reflects elevated-temperature capability, and corrosion reflects resistance in general industrial environments. Actual performance depends on powder quality, particle size, additive-manufacturing process, heat treatment, and service conditions.
Compare 15–45 μm LPBF with 45–106 μm DED Particle-Size Targets
Choosing alloy powder starts with the deposition process, not the alloy name. LPBF commonly targets 15–45 μm particles, while DED often uses 45–106 μm powder. These ranges are practical, not universal rules.
For LPBF, finer particles can improve layer coverage and packing. They also increase dust, moisture sensitivity, and electrostatic behavior. A 25 μm particle may spread smoothly, yet satellites can disturb recoating. DED needs stronger flow through a feeder and nozzle. Larger particles usually reduce clogging risks and support stable powder delivery. However, excessive coarse material can produce rough surfaces and uneven melt tracks. It is a trade-off.
Measure the distribution, not only the nominal range. ISO/ASTM 52907 recommends evaluating powder morphology, chemistry, size distribution, flowability, and density. ASTM B213 Hall-flow testing can reveal feeder behavior, but test results may change after handling. Screened powder is not automatically consistent powder. Check oxygen, nitrogen, moisture, and satellite content between batches. Traceability matters.
The Wohlers Report 2024 valued the global additive manufacturing market at approximately $20.035 billion in 2023. That scale makes powder qualification more important, not less. Use a small build or deposition trial before purchasing volume. Record spread quality, feed rate, recovery, and surface finish. My practical mistake was trusting a size label too quickly. Machine settings, alloy shape, and recycling history can overturn the specification. Validate the powder on your equipment.
Assess Flow and Packing with ASTM B213 50 g and ASTM B212 Tests
How to Choose the Right Alloy Powder for Your Needs?
Alloy selection should begin with measurable powder behavior, not chemistry alone. ASTM B213 evaluates flow rate through a Hall flowmeter using a 50 g sample. This small, defined quantity reveals how consistently powder moves through a calibrated funnel. Record the discharge time in seconds, and repeat the test under controlled conditions. A powder that bridges, pulses, or leaves residue may create unstable feeding during production.
ASTM B212 measures apparent density using a Hall flowmeter. It shows how loosely the particles occupy a known volume before pressing or sintering. Fine particles may produce higher surface area but pack differently from spherical particles. Particle shape, size distribution, moisture, and surface oxides can all change the result. Keep the funnel clean, use a dry container, and handle the powder gently. Small details matter.
Test more than once. Three or more readings can expose variation between samples. A single smooth result can mislead. Compare flow time and apparent density together, rather than choosing powder from one number. High density does not always mean easy feeding, and fast flow does not guarantee uniform packing. Document temperature, humidity, sample condition, and operator technique. The method is dependable, but the interpretation still needs judgment. Manufacturers should confirm these laboratory results with actual equipment trials before approving an alloy powder.
Verify Reuse, Traceability, and Cost Using ISO/ASTM 52907 Lot Controls
How to Choose the Right Alloy Powder for Your Needs?
Alloy selection starts with lot control, not a glossy datasheet. ISO/ASTM 52907 recommends documenting metal powder characteristics, test methods, and material identity. Ask for a unique lot number, certificate of analysis, particle-size distribution, chemistry, morphology, oxygen, and moisture data. Record the supplier lot beside every build job.
Reuse needs stricter evidence. Label each container with opening date, machine, number of thermal exposures, sieving results, and remaining mass. A fresh-looking powder may still contain satellites, agglomerates, or changed oxygen levels. In production reviews, separating virgin and reused powder prevents a cheap blend from becoming an expensive investigation. Keep samples for later testing. Small details matter.
Cost calculations should include screening, storage, testing, disposal, and failed builds. The Wohlers Report 2024 valued the global additive manufacturing industry at approximately 20.0 billion US dollars in 2023, increasing pressure to control material waste. Yet the lowest purchase price can mislead. Compare cost per accepted part, not cost per kilogram. I would not claim every reuse cycle is predictable; powder behavior depends on alloy, machine atmosphere, exposure, and process settings. Traceability makes that uncertainty visible, while weak records leave operators guessing.

